
Welding rotators look simple from a distance: two sets of wheels, a frame, a drive. Yet the specification sheet behind them decides whether a fabrication shop produces consistent circumferential welds or spends its days chasing arc wander and rework. Buyers who treat capacity, rotation speed, and control as three independent checkboxes often end up with a machine that either stalls under a heavy vessel or turns too fast for a delicate root pass. The three variables are interdependent — load determines wheel loading, wheel loading constrains available torque, and torque sets the usable speed range under control. This guide walks through each specification in the order a buyer should evaluate it, with the practical checks that separate a rotator that runs for fifteen years from one that disappoints in six months.
Capacity is quoted as a single tonnage figure, which makes it the easiest spec to compare and the easiest to misread. That figure normally assumes the workpiece center of gravity sits close to the rotational axis, with the load shared evenly between the two wheel sets. Real vessels rarely cooperate.
A shell with a heavy nozzle cluster, an offset manway, or internal baffles shifts the center of gravity away from the axis, and the load on one wheel set rises while the other drops. For eccentric or asymmetric workpieces, effective wheel loading can exceed the nominal figure by 15 to 25 percent. Rather than applying a blanket derating factor, send the supplier your actual part drawing and ask for a wheel-load calculation. A reputable manufacturer will run that number before quoting, not after the machine is on your floor.
Also confirm whether the rating applies to the rotating load alone or includes tooling, fixturing, and a welding head mounted on the frame. Accessories add weight that the drive still has to turn.
Wheels are where capacity becomes physical. Three decisions matter:
BOTA sizes wheel sets and wheelbases against part drawings rather than catalog ranges, because a rotator that technically fits a diameter but contacts the shell at the wrong angle will slip under load.
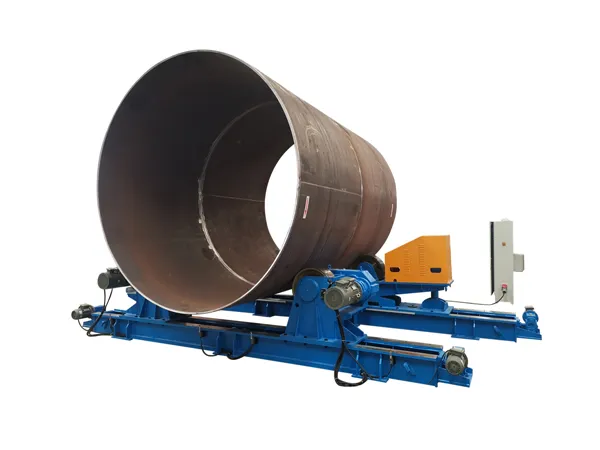
Most circumferential welding falls somewhere between roughly 0.1 and 1.0 rpm, but the top speed on a datasheet tells you very little. The number that matters is the lowest stable speed the unit can hold under full load without stalling, surging, or cogging.
A fixed-speed rotator suits one repetitive job and nothing else. As soon as your workpiece diameter, wall thickness, or process changes, travel speed has to change with it. Three drive approaches dominate the market:
Ask for a torque curve, not just a horsepower rating. A drive that turns 5 rpm freely may stall at 0.2 rpm with a 20-ton vessel on the wheels. Look at the turn-down ratio — the span between maximum and minimum controllable speed — and confirm that the low end is rated at full load. If the answer is vague, the low-speed performance probably is too.
...
For more detailed information on selecting welding rotators—covering capacity, speed, and controls—please click here: https://www.bota-weld.com/en/a/news/welding-rotator-buying-guide.html