
Selecting a welding rotator for heavy pipe fabrication is a capacity and safety decision, not a catalog exercise. A rotator that is undersized for a large-diameter spool will slip, vibrate, and pull the weld seam out of position; one that is oversized wastes floor space, power, and capital. The variables that matter most are the actual load carried by each wheel, the pipe diameter range you plan to run, the drive configuration, and how precisely rotation speed must match your welding process. This guide follows the specification decisions in the order most fabrication shops make them, from load calculation through control system selection, and explains where a supplier's engineering support makes a measurable difference to throughput and weld quality.
Catalog capacity ratings describe a balanced, static load. Real pipe fabrication rarely looks like that. Before you compare models, work out what each rotator will actually carry during the heaviest job you expect to run.
A practical rule: calculate the worst-case total, then apply a working safety margin instead of buying exactly at the rated figure. Where a long pipe spans two rotators, remember the load is not split evenly — an off-center fitting can push most of the weight onto one unit. If you cannot confidently determine the distribution, ask the supplier to review the pipe drawing rather than guessing.
A rotator used for occasional fit-up and tacking has different requirements from one running continuously under a submerged arc or narrow-gap welding head. Continuous rotation at low speed for hours heats the motor and gearbox, and it demands a drive rated for that duty cycle. State your expected hours per shift and whether the rotator will run unattended for long welds.
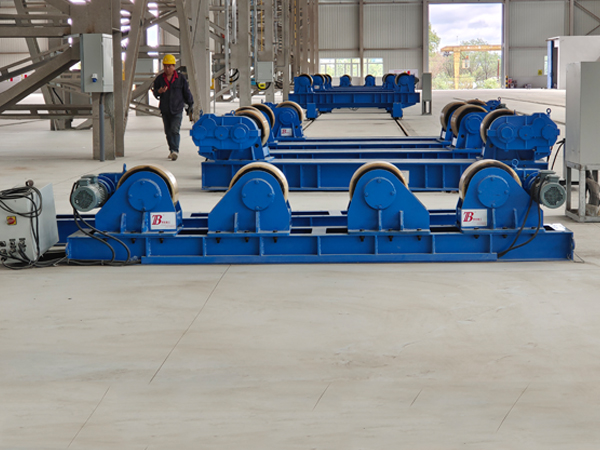
Capacity is only half the specification. Diameter range determines wheel spacing, frame geometry, and whether the rotator is adjustable at all.
Two details cause most problems. First, running small-diameter pipe on a rotator sized for large diameters raises the pipe too high and can cause the wheels to lose contact under load. Second, rotation speed for welding is normally set as surface speed, not RPM — a small pipe and a large pipe at the same RPM rotate at very different linear speeds. Confirm the rotator's speed range covers the surface speed your welding procedure requires at both ends of your diameter range.
The drive arrangement determines torque, tracking, and how easily the pipe stays aligned with the weld head.
For heavy pipe fabrication, dual-drive synchronous rotation is rarely optional. Mismatched rotation between a powered rotator and a passive idler introduces torsional stress and drift that shows up as inconsistent penetration and bead appearance.

Wheel selection affects grip, marking, and pipe finish. Polyurethane wheels protect stainless, aluminum, and coated pipe from contamination and surface damage. Steel wheels handle the heaviest loads and high temperatures but can mark softer material. Rubber or composite wheels sit between the two and suit general carbon steel work. Check wheel diameter as well: larger wheels reduce contact pressure and roll more smoothly over longitudinal seams and weld caps, which matters when the pipe surface is not perfectly round.
...
For more details on how to select the right welding rotator for heavy-duty pipe fabrication, please click here: https://www.bota-weld.com/en/a/news/welding-rotator.html